
The Allowance · Craft Notebook
How a bell is made
Core, cope, and strickle; the pour and its real hazards; cooling, breakout, and tuning; how a cast bronze shape becomes a hung, sounding instrument.
- Level
- Beginner
- Reading time
- 14 minutes
- Evidence
- craft-and-standards
- Reviewed
- 2026-08-09
Jump through this guide
The short version
A bell is not carved or printed into its final voice; it is cast rough and finished by removal. This notebook follows the classic route from the two-part mould, a core and a cope raised to a profile swept by a rigid template called a strickle, through the pour, cooling, and breakout, to the tuning that cuts a deliberate reserve of metal away, and finally to the headstock and clapper that let a casting become an instrument. Bell acoustics researcher Bill Hibbert and conservation writer David J Kelly document the trade's shape logic and tuning history; Notre-Dame's own record of its bells supplies scale and stakes.
After reading, you can
- Describe how a bell's core and cope set its inner and outer profile before any metal moves
- Explain why uniform wall thickness, not decoration, governs a bell's tone
- Identify the real hazards of a bronze pour and the safety practice that governs metal casting operations
- Trace a bell's path from breakout through tuning to a hung, sounding instrument
01
Two moulds make one bell
Bell founding starts with geometry, not metal. A bell mould is built in two parts: a core, which forms the bell's inner surface, and a cope, which forms the outer surface. The gap held between them, precisely maintained on every radius, becomes the wall of bronze that will ring. That shape is traditionally raised in the foundry itself rather than carved freehand, built up and swept to a fixed profile with a rigid template called a strickle, turned around a fixed spindle so every pass repeats the same curve. Bell acoustics researcher Bill Hibbert notes that each bellfounder kept his own shape for bells, determined by strickles or layout rules passed down across generations from a founder to his apprentices, sometimes barely changing for decades because a strickle was only remade when it wore out 1.
Getting the two mould halves aligned is not a finishing touch, it is the whole job. A conservation survey of English church bells found that most founders realized a lack of uniformity in a bell's shape had a considerable effect on sound quality, and were careful that the inner and outer moulds were precisely positioned to give uniform thickness around the bell's circumference; castings with non-uniform thickness sound very poor and were generally the mark of a poor founder 2. The core sits inside the cope like a second skeleton, and the constancy of the space between them is the one dimension a founder fully controls before the fire is ever lit.
02
Why thickness decides the sound before the pour does
A bell's tone is not added after casting, it is set into the mould's geometry. Hibbert's acoustic research shows that wall thickness, especially at the soundbow, the thickest part of the bell near where the clapper strikes, controls the spacing of the rim partials, the family of overtones that, together with the low hum, prime, tierce, quint, and nominal partials, build the sound a listener hears. A thicker bell compresses its rim partials together; a thinner bell stretches them apart, and either shift also moves the strike note, the pitch a listener actually perceives, which is generated in the ear and brain and may not correspond to any single frequency physically present in the bell's sound 1.
This is why a strickle's profile is an acoustic decision made in advance of a process that cannot be argued with once it starts, not a stylistic signature. Early founders worked mostly by trial and inherited habit; the underlying relationships between the low partials were not explained scientifically until analysis in the 1890s showed how they could be brought into octave, or true-harmonic, relationships, a discovery that arrived centuries after the moulding skill it depended on 12.
03
The pour, and why it ends most conversations
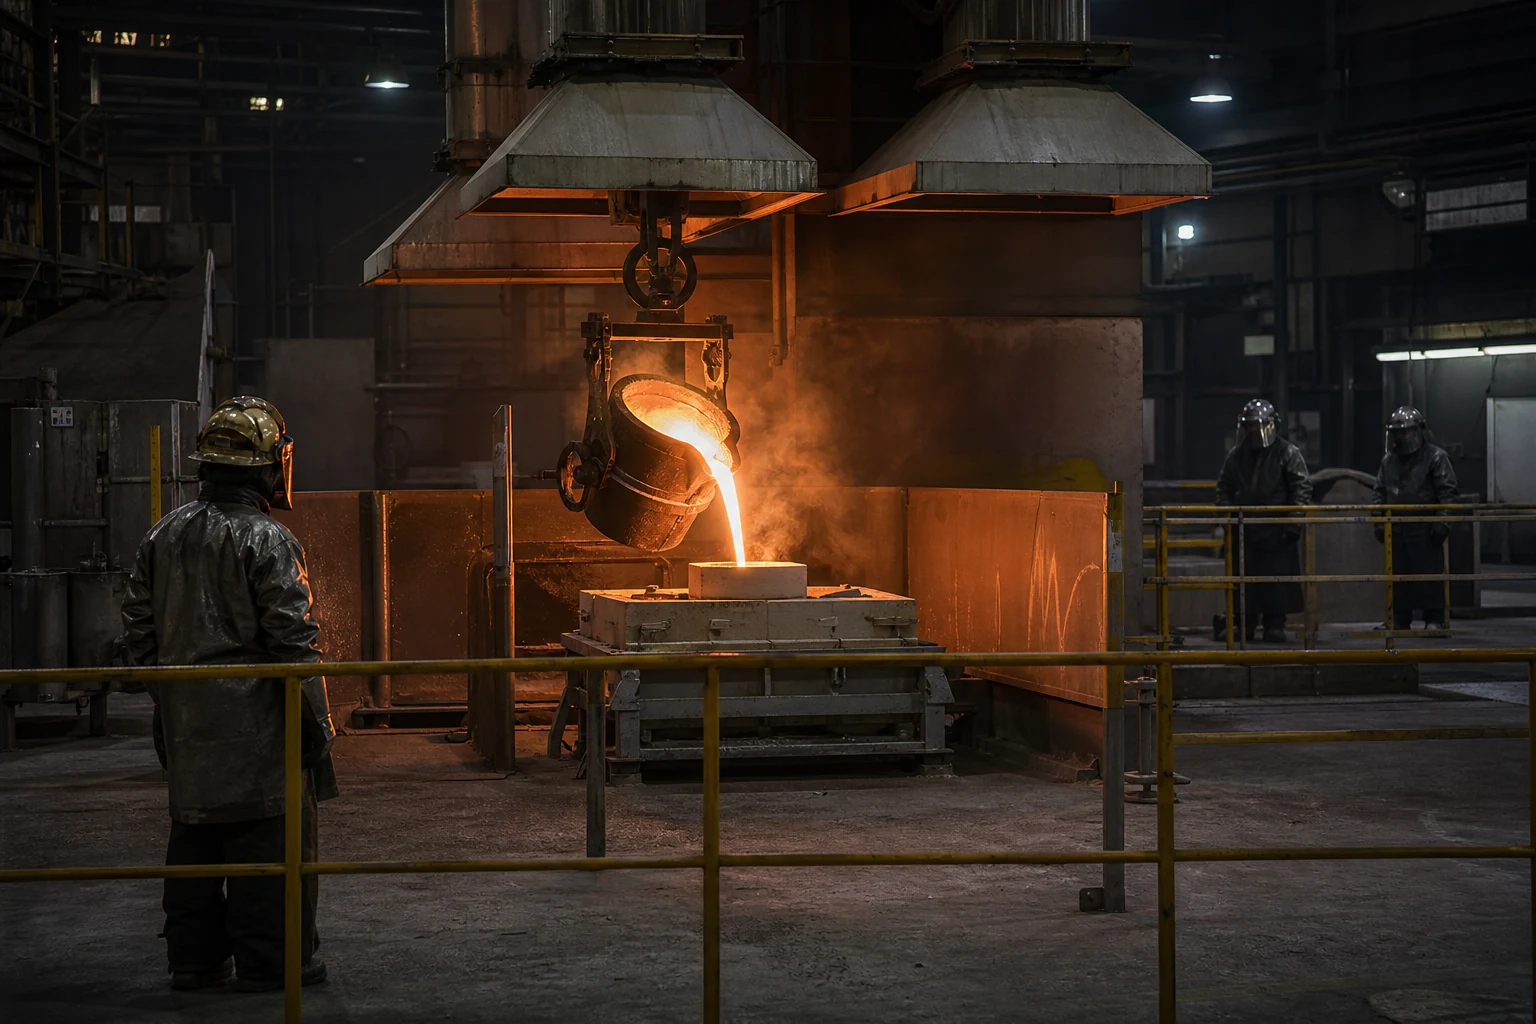
When the assembled mould is ready, molten bronze, an alloy of copper and tin, is poured to fill the cavity between core and cope in a continuous flow. This is the least forgiving moment in the trade: a stalled or split pour, trapped moisture, or a mould that shifts under the weight of liquid metal can ruin a casting or injure anyone standing near it. Metal casting operations covering sand preparation, moulding and core making, melting and pouring, and cleaning and finishing are governed by dedicated industrial safety practice precisely because the heat, the machinery, and the mass involved leave little margin for improvisation 4.
Cooling follows the mould's schedule, not the calendar's. A casting must lose heat gradually enough that the bronze does not crack under its own contraction, and only once it has cooled is breakout possible: the process of freeing the bell by removing the mould material around it. A single-use mould does not survive its own bell, it is destroyed to release the very shape it created, which is one reason a founder's strickle, not any individual mould, is the object worth guarding across generations.
04
Breakout is the beginning of judgment, not the end of the job
A bell fresh from breakout is rough: it carries mould marks, an as-cast surface, and a wall that a careful founder has cast slightly thicker than the acoustic target requires, on purpose. That extra thickness is a tuning reserve, deliberate margin left for a tuner to remove later, because a founder can control the mould's shape but cannot fully predict the finished bell's sound from geometry alone, and because metal taken off a bell can never be put back 12. Before the close of the 19th century, tuning meant a hammer, chisel, and file worked mostly at the soundbow and lip; large vertical boring machines introduced late in that century let a tuner cut precisely from almost any part of a bell's interior 2. A companion guide in this series, The tuning reserve, follows that allowance in detail.
The build order is short to state and unforgiving to run.
- Core and cope raised to a fixed strickle profile
- Mould assembled, core positioned inside cope
- Molten bronze poured to fill the gap between them
- Cooling on the metal's own schedule, not the founder's
- Breakout: the mould is destroyed to free the casting
- Tuning: the reserve is cut away by hand or on a lathe
05
From casting to a hung, sounding instrument
A cast and tuned bell is still not an instrument until it is mounted. The headstock, a heavy timber or steel beam, carries the bearings that let the bell swing, and inside it a separate hammer called the clapper hangs from the crown, striking the soundbow as the bell passes through the vertical. The headstock and its bearings, not the bronze alone, are what let a multi-tonne casting move safely and repeatably for generations of ringing.
Scale varies enormously, and so does the engineering it demands. Notre-Dame's bourdon Emmanuel, cast in 1683 and named for its royal godfather Louis XIV, rings in F-sharp from a base diameter of 2.62 metres and a wall 21 centimetres thick, and weighs 13 tonnes complete with a 500-kilogram clapper; it was the only bell spared when the cathedral's other bells were taken down and melted during the Revolution in 1791 and 1792 3. Every part of that assembly, core and cope, pour and breakout, tuning reserve and clapper, traces back to the same two mould halves a founder aligned before any metal moved.
Working vocabulary
Glossary
- Core
- The inner part of a bell mould, shaping the bell's inside surface.
- Cope
- The outer part of a bell mould, shaping the bell's outside surface; the gap between core and cope becomes the bell's wall.
- Strickle
- A rigid template swept around a fixed spindle to raise a mould to a founder's inherited profile.
- Soundbow
- The thickest part of a bell's wall, near where the clapper strikes, most influential on tone.
- Breakout
- Freeing a cooled casting by removing the single-use mould material around it.
- Tuning reserve
- Extra metal deliberately cast into a bell so a tuner can remove material later without falling short.
- Headstock
- The heavy beam and bearing assembly that carries a bell so it can swing.
- Clapper
- The internal hammer, hung from a bell's crown, that strikes the soundbow to sound the bell.
Source ledger
References and further study
Numbered citations point to the sources below. We favor standards, government laboratories, peer-reviewed research, and primary technical documentation. A link is evidence for the claim it supports—not an endorsement of every claim on that website. Read the full editorial and correction method.
- Building a bell soundBill Hibbert, The Sound of Bells · bell acoustics research and craft history↗Opens in a new tab
- Church Bells in TrustDavid J Kelly, Cathedral Communications, Historic Churches · conservation trade publication↗Opens in a new tab
- The BellsCathédrale Notre-Dame de Paris · cathedral institutional record↗Opens in a new tab
- Standard Practice for Safety Requirements in Metal Casting Operations: Sand Preparation, Molding, and Core Making; Melting and Pouring; and Cleaning and FinishingASTM International · industrial safety standard↗Opens in a new tab